


Stone countertops are high-density, high-value building materials with strong compressive strength but weak impact resistance at edges and corners. During international transportation, vibration, stacking pressure, humidity changes, and forklift handling create multiple failure points that must be controlled through engineered packaging systems.
Packaging is not a secondary process. For countertop export, it is a structural engineering component directly linked to breakage rate, installation delay, and project cost.
Why Stone Countertop Packaging Matters in Global Shipping
Stone countertops such as marble, granite, quartzite, and quartz are commonly fabricated with:
- Thickness tolerance: ±10 mm to ±1.0mm
- Surface finish: Polished / Honed / Leathered
- Edge type: Eased edge / Bullnose / Mitre edge
- CNC precision cutting for sink openings and profiles
- Despite high compressive strength, natural stone is vulnerable under:
- Point impact on edges
- Corner collision during handling
- Vertical stacking pressure inside container
- Moisture expansion during long sea freight
- Repeated forklift repositioning
Common shipping failure modes
| Damage Type | Root Cause | Typical Stage |
|---|---|---|
| Edge chipping | Poor corner protection | Loading/unloading |
| Surface scratches | Lack of isolation layer | Packing stage |
| Crack formation | Internal vibration | Ocean freight |
| Warping stress | Uneven support base | Container stacking |
| Moisture stains | No waterproof barrier | Sea transit |
Even materials with Mohs hardness 6–7 (granite, quartzite) can still suffer edge failure if packaging structure is not properly designed.
Packaging Systems for Stone Countertops
Global countertop buyers generally operate two distribution models:
Retail distribution (single unit sales)
Project-based bulk supply (construction shipment)
Each requires a different packaging engineering approach.
Retail Carton Packaging for Supermarkets and Home Improvement Stores
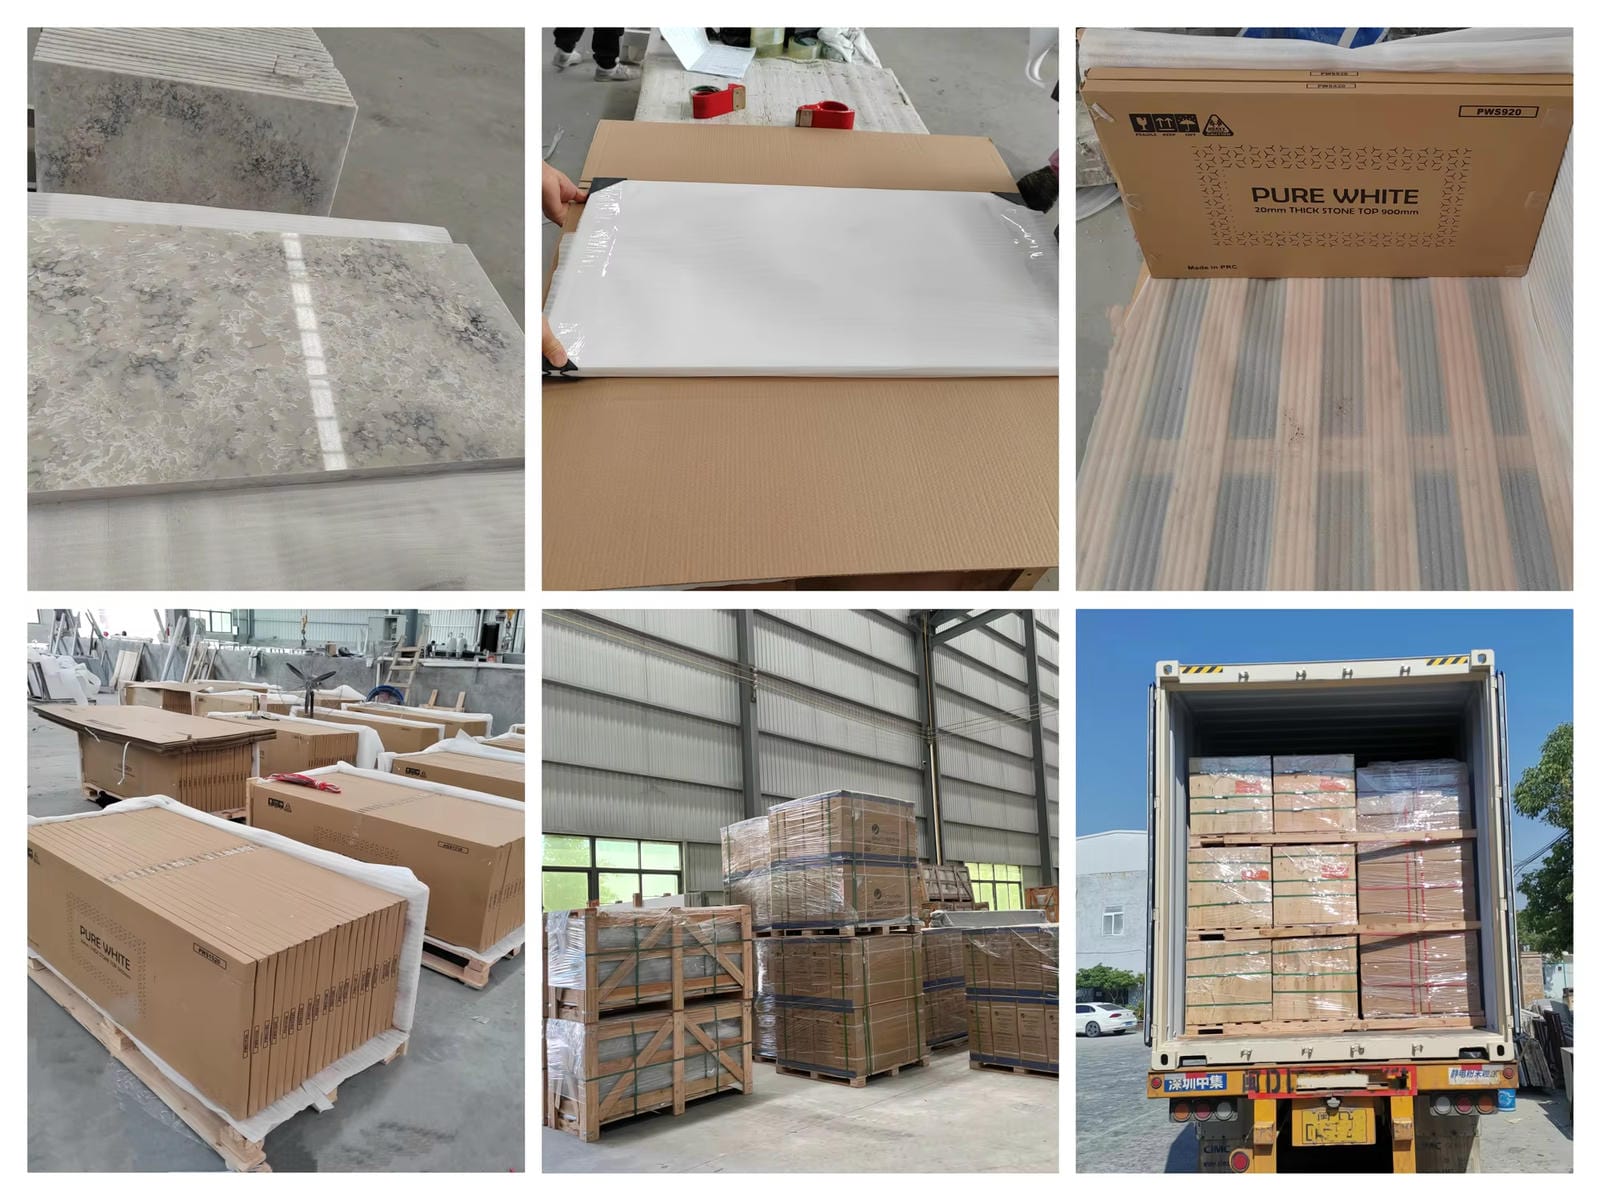
Retail packaging is designed for individual sale units where each countertop is handled multiple times before installation.
Packaging structure for retail units
Each countertop is packed individually using:
- Shock-resistant corrugated carton
- High-density EPS/EPE foam cushioning
- Anti-scratch protective film wrapping
- Edge and corner protectors
- Customizable Product barcode + SKU labeling
- Optional OEM retail branding carton
Retail packaging functional advantages
- Independent unit traceability
- Shelf-ready warehouse storage
- Reduced handling damage during retail logistics
- Faster inventory scanning and stock rotation
- Suitable for e-commerce fulfillment channels
Export Wooden Crates for Wholesale and Construction Projects
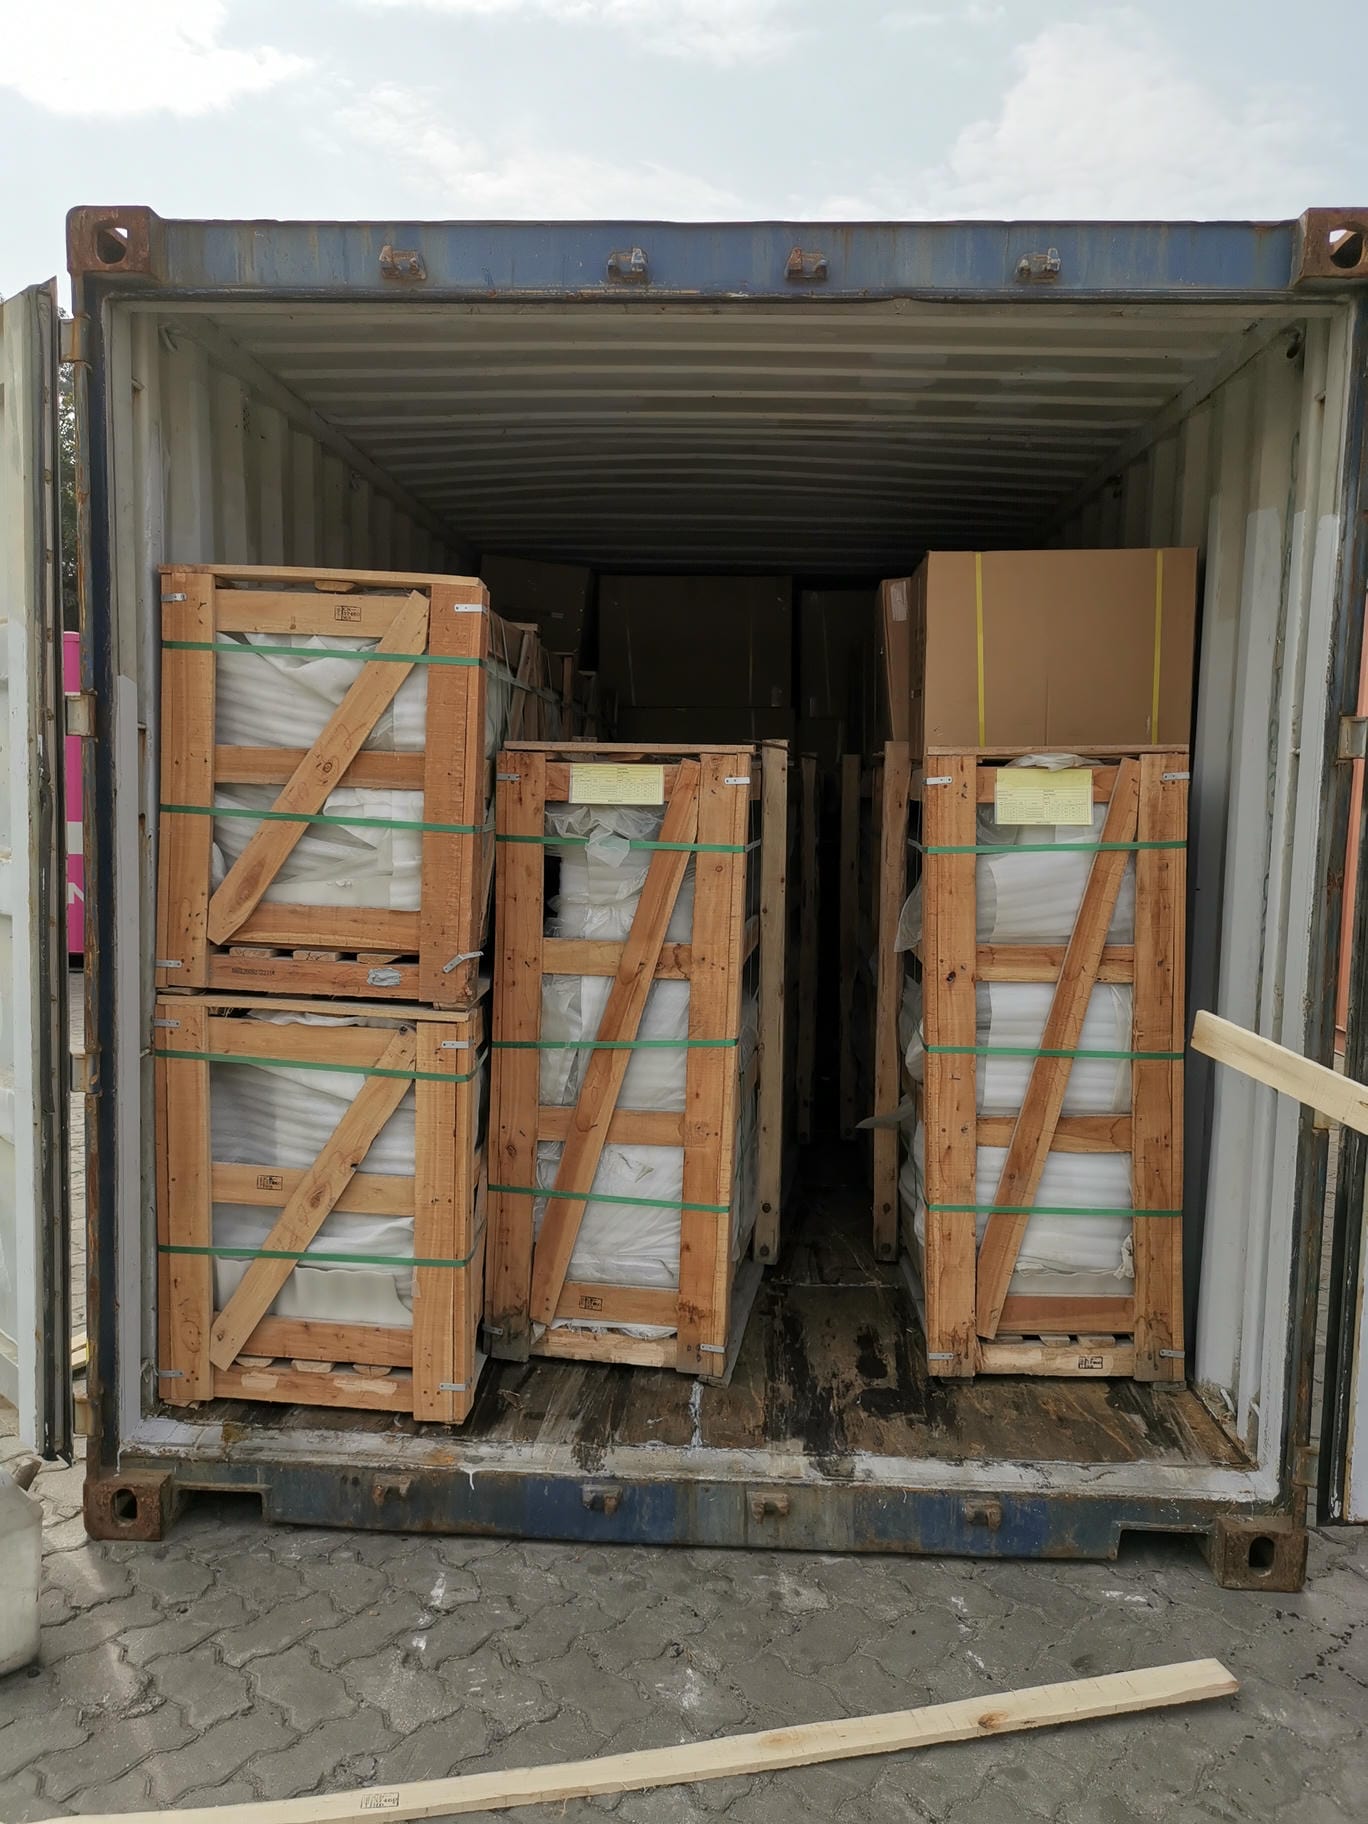
For bulk shipments, countertop products are packed directly into export-grade wooden crates without individual retail cartons.
This system is used when packaging efficiency and container utilization are more important than retail presentation.
Typical project applications
- Apartment construction projects
- Hotel renovation projects
- Commercial building installations
- Builder supply contracts
- Wholesale distribution shipments
Crate packaging structure
- Plywood or solid wood crate base
- Internal wooden blocking system
- Foam separation layers between slabs
- Fixed anchoring points for movement control
- Forklift-accessible pallet base
Advantages of wooden crate packaging
- Higher container loading efficiency
- Lower per-unit packaging cost
- Faster on-site unloading
- Reduced handling steps
- Better suited for mass installation schedules
Stone Countertop Customized Packaging Solution
Stone products vary significantly in size, thickness, and fragility depending on material type:
- Marble: lower density, higher fracture sensitivity
- Granite: high hardness, moderate edge chipping risk
- Quartzite: high density, brittle fracture behavior
- Quartz: engineered uniform structure, controlled fragility
Because of these differences, standardized packaging is not sufficient for all shipments.
Customized packaging systems consider:
- Product dimensions (cut-to-size vs standard slab)
- Weight distribution per crate
- Container type (20GP / 40HQ)
- Destination climate conditions
- Retail vs project supply chain
Reinforced Wooden Crates for Tall and Oversized Stone Countertops
When crate height exceeds standard structural limits, additional reinforcement is required to prevent deformation during stacking and vibration.
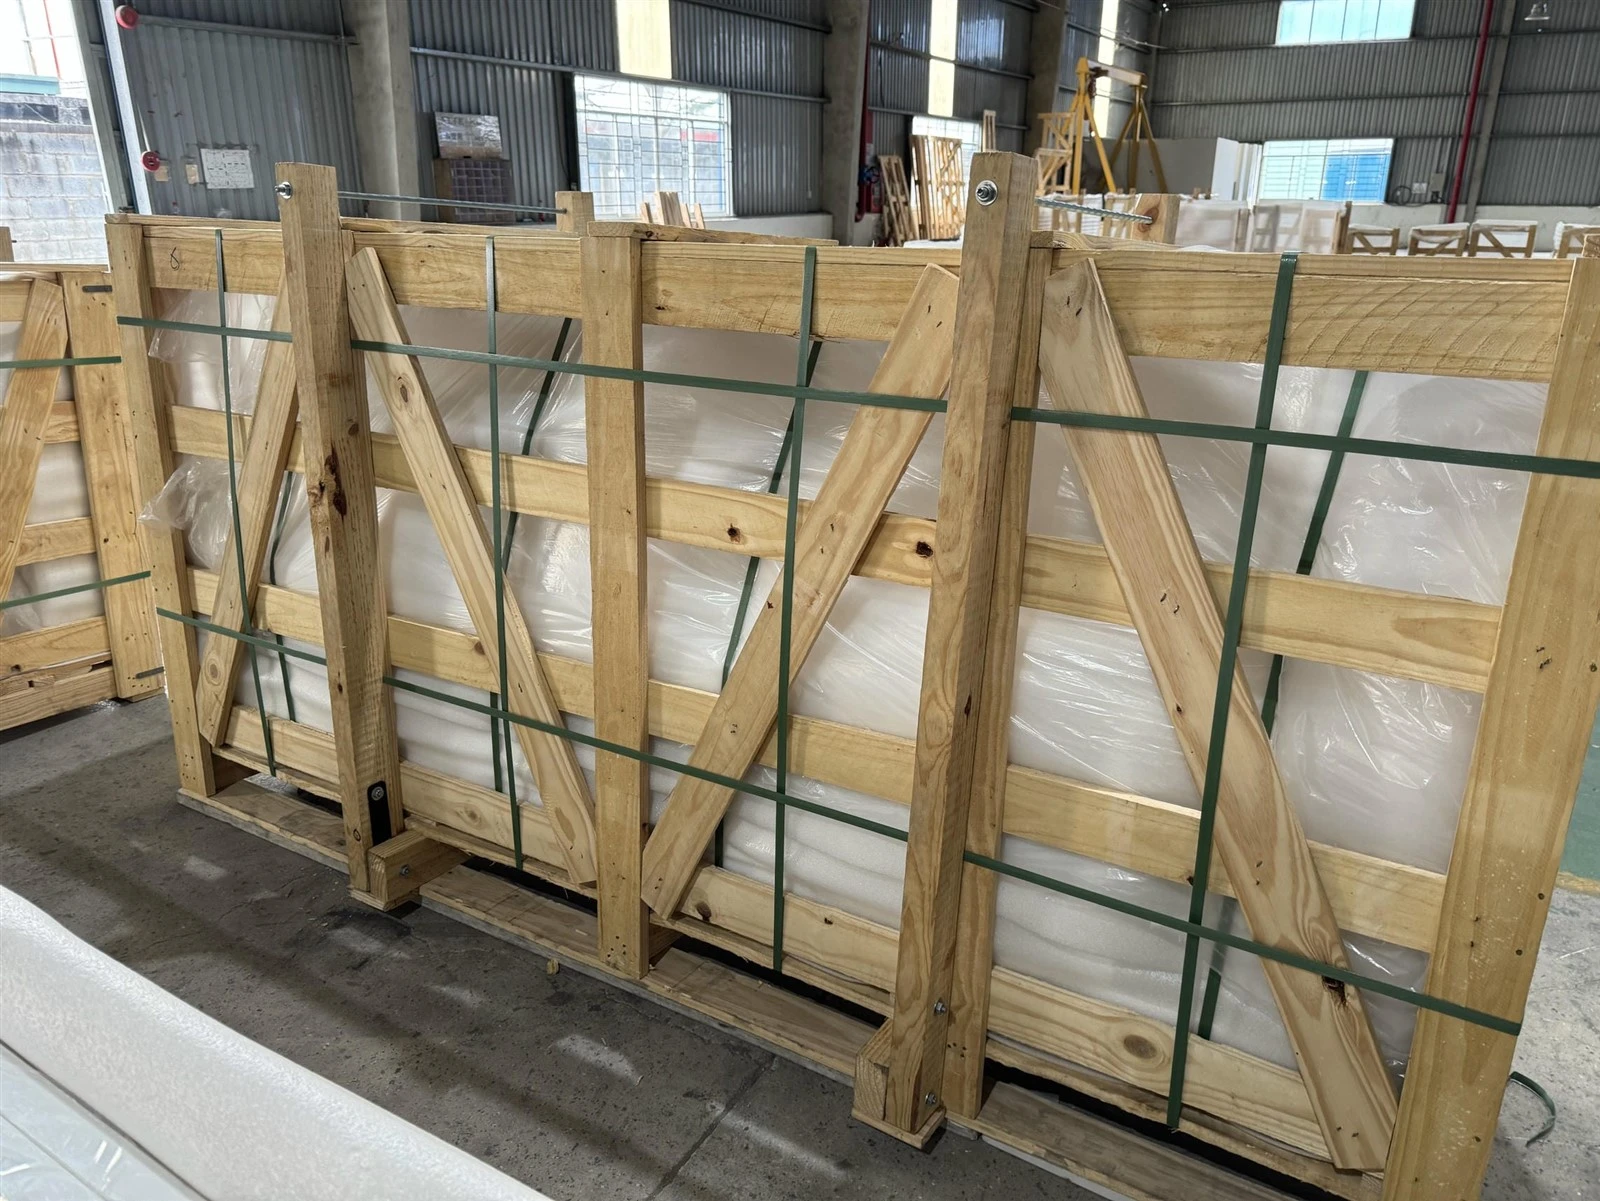
Reinforcement structure options:
Internal vertical timber support frame
Steel cross-bracing system
Horizontal load distribution beams
Base forklift reinforcement platform
Anti-flex deformation locking system
Engineering purpose:
Prevent crate wall deformation under stacking load
Reduce vibration transmission during sea freight
Maintain slab vertical stability during container movement
Improve compression resistance under multi-layer stacking
Concerned about breakage risk in tall export wooden crates during ocean shipping?
Request Export Packaging Engineering Plan

Anti-scratch and Shock Protection System Overview
Stone countertop packaging requires multi-layer protection logic rather than single-material reliance.
Core protection mechanisms include:
Surface isolation film to prevent micro-scratches
Foam cushioning to absorb vibration energy
Corner reinforcement to reduce impact stress concentration
Internal blocking to eliminate movement inside crate
Moisture barrier for long ocean transit stability
These layers work together to reduce cumulative transport stress during multi-stage logistics operations.
Export Experience Across USA, Canada, and Australia Markets
Stone countertop packaging standards vary significantly across different regions due to logistics infrastructure, retail structure, and construction procurement models.
| Region | Characteristics |
| North America (USA & Canada) |
Typical requirements:
Common applications:
|
| Australia & New Zealand |
Key requirements:
|
| Middle East (UAE / Saudi Arabia / Qatar) |
Key characteristics:
|
Across all regions, packaging design is adjusted based on:
- Installation schedule urgency
- Import handling conditions
- Retail vs project supply chain model
The core engineering principle remains consistent: packaging must match transport stress, not just product appearance.
One Packaging System Does Not Fit All Countertops
Stone countertop packaging must be segmented based on business model:
| Business Model |
Packaging |
| Retail distribution |
Individual carton packaging Barcode labeling system Shelf-ready retail units High handling frequency protection |
| Wholesale distributors |
Mixed carton + crate hybrid system Batch identification packaging Container optimization focus |
| Construction projects |
Bulk reinforced wooden crate packaging High stacking strength design Fast unloading priority |
| OEM / brand customers |
Custom carton printing Logo integration Retail-ready packaging design Customized crate engineerin |


Why Wholesale Buyers Choose Guanmay Stone Packaging System
Guanmay's countertop packaging system is designed based on export data from long-term shipments to North America, Australia, and Middle East markets.
Core capabilities:
- Retail-ready individual carton packaging
- Reinforced export wooden crate systems
- Extra bracing frame design for tall crates
- Anti-scratch and shockproof multi-layer protection
- Moisture-resistant long-distance sea freight packaging
- Container loading optimization engineering
- OEM customized packaging solutions
- Project-based packaging configuration support
Each packaging design is selected based on:
- Material type (marble, granite, quartzite, quartz)
- Product geometry (slab, vanity top, island top)
- Shipment destination
- Container type
- Handling environment

FAQ
Why do stone countertops require different packaging systems for retail and project shipments?
Retail shipments require individual carton protection for repeated handling and shelf display. Project shipments prioritize bulk efficiency and use reinforced wooden crates to maximize container utilization and reduce unloading time.
What is the function of extra bracing frames in tall wooden export crates?
Extra bracing frames prevent structural deformation during stacking and ocean freight vibration. They distribute vertical load evenly, reduce sidewall pressure, and maintain slab alignment inside the crate.
Can moisture affect marble countertops during sea freight even when packed?
Yes. High humidity environments can cause temporary surface darkening or moisture absorption if waterproof barriers are insufficient. Proper sealed wrapping and crate moisture control significantly reduce this risk.

Complete Stone Countertop Packaging Solution & Engineering Support
Send your project specifications, CAD drawings, or container plan to receive:
Packaging structure recommendation/ Container loading layout plan/ Retail vs project packaging configuration/ OEM packaging customization options